Spring Cable Winding Machine for PU Spiral Power Cables
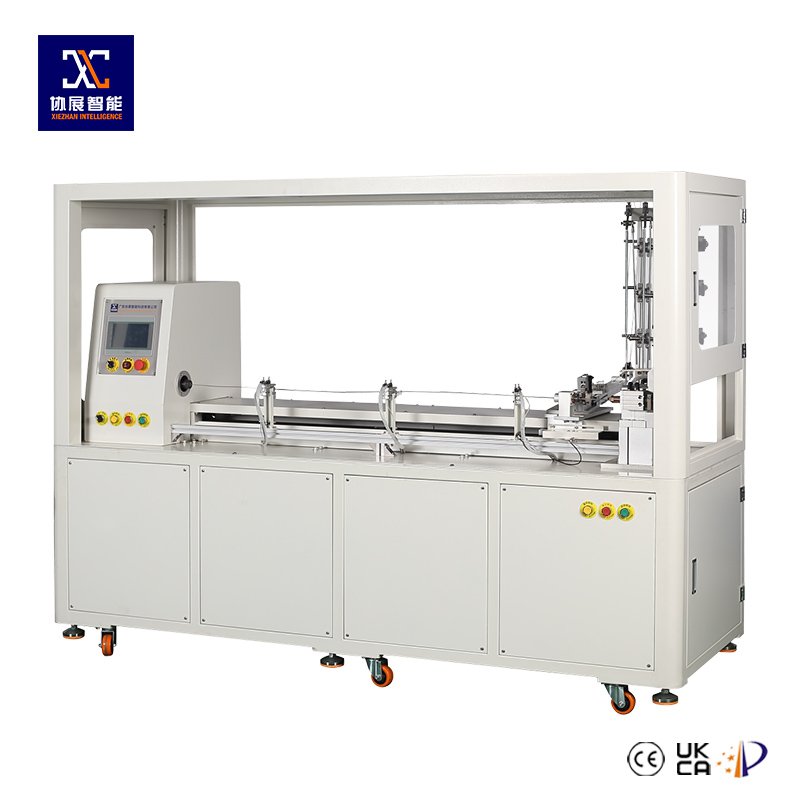
Spring Cable Winding Machine
Most spiral cable complaints don’t show up on delivery day. They show up three or four months later, when an end customer reports that the coil has gone slack, or the cable no longer pulls back after being stretched, or a device stops charging because a conductor has broken somewhere inside the spiral. By then the cables are shipped, invoiced and installed, and the winding machine that formed them is the last thing anyone suspects. That timeline is worth keeping in mind before you compare quotations, because it changes what you should be looking for in a spring cable winding machine.
Why a Good-Looking Coil Proves Very Little
A freshly wound coil looks the same whether the process behind it is sound or marginal. The pitch is even, the diameter is right, the surface is clean. What buyers actually pay for is something else: how the cable retracts, how long it keeps its shape, how many pulls it survives. Those qualities are decided by two things you can’t see on the bench, namely how heat was applied to the insulation and how much stress the copper strands took while the cable was being formed.
That is why two machines can produce coils that are indistinguishable on a table and behave completely differently in a customer’s hands. If you are comparing a few winding machine options for spiral cable production, it helps to ask what the machine does to the cable rather than what the finished coil looks like.
Heat and Cooling: The Part That Decides Shape Memory
A spiral cable holds its shape because the insulation is warmed while it is wrapped and then cooled while it is still held in position. Get that sequence right and the coil remembers its form. Get it slightly wrong and the problems arrive slowly. With too little heat, or heat that is uneven along the cable, the coil relaxes over the following weeks. A buyer sees this as coils that measure fine at inspection and look loose after storage. With too much heat, the insulation surface can soften, pick up marks from whatever it touches, or pass stress on to the conductor underneath.
Cooling matters just as much and gets discussed much less. If the coil is released before the insulation has stabilised, it springs open a little, and the diameter you measured on the machine is not the diameter you ship. The question worth putting to any supplier is a plain one: what holds the coil in place while it cools, and for how long?
What Happens to the Conductor Inside
Inside the insulation there are usually many fine copper strands, and they are less forgiving than the jacket around them. Forming a spiral bends and twists the whole cable, and if tension runs high or drifts during a long run, the strands are pre-stressed before the cable ever leaves the factory. Nothing looks wrong, and continuity passes at final inspection. The damage appears only after thousands of stretch-and-release cycles, when a stressed strand finally gives way.
This is why tension control deserves more attention than it usually gets in quotations, where it tends to appear as a single line. Steady tension across an entire production run, not just the first few minutes, is what protects the conductor. Ask how tension is held constant as the reel diameter changes, because that is where many machines quietly lose consistency.
The table below pulls these points together. It is less a checklist than a way to connect a complaint you might receive later with a question you can ask now.
| Complaint You Might Get Later | Likely Cause During Forming | What You See at Sample Stage | How to Check It Yourself | Question for the Supplier |
|---|---|---|---|---|
| Coil goes slack in storage or use | Heat setting too low, or uneven along the cable | Coil looks perfect straight off the machine | Leave samples for a week, then re-measure diameter and pitch | “How is heat applied, and how long is the hold time?” |
| Cable won’t retract after stretching | Coil released before the insulation stabilised | Slight opening after a first pull | Stretch to working length repeatedly and compare resting length | “What holds the coil in shape while it cools?” |
| Conductor breaks inside the spiral | Excess or drifting tension pre-stressed the strands | Nothing visible, continuity passes | Flex-cycle a few pieces, then test continuity again | “How is tension held steady through a full run?” |
| Surface marks or dull patches | Overheating or contact pressure at the forming point | Faint marks visible only at an angle | Inspect under raking light along the whole length | “What actually touches the cable during forming?” |
| Diameter drifts across a long batch | Feed and cooling not stable over time | Early coils fine, later coils differ | Measure coils from the start, middle and end of one run | “Can I see a long-run sample, not a short one?” |
One pattern worth noticing: these problems are very often blamed on the cable material when they turn up in the field. That is understandable, since the coil is the visible part. But a supplier who has actually traced failures back through production will usually tell you the forming process was the cause more often than the compound was.
PU and PVC Do Not Forgive the Same Mistakes
Polyurethane cable has good elastic recovery and tolerates repeated stretching well, which is why it dominates spiral cable work. It also gives you a wider margin for error during forming. PVC is usually chosen for cost, but it recovers less completely and its workable temperature window is narrower, so a heat setting that suits PU can leave PVC either under-set or marked. If your product line includes both, it is fair to ask how the machine is adjusted between them and how long a changeover realistically takes, rather than accepting “compatible with both” at face value.
A Trial Routine That Costs Little and Says a Lot
Before committing to an order, the most useful thing you can do is send your own cable for a trial, not the supplier’s preferred sample cable. Then run a few simple checks yourself. Measure coil diameter and pitch when the samples arrive, and again after they have sat for a week. Stretch several coils to their working length repeatedly and see whether they return to the same resting length. Then flex-test a few pieces and check continuity afterwards, since a break inside the spiral is exactly what an early visual check will miss.
The numbers that count as acceptable should come from your own end customer’s requirement, not from a general rule. An automotive charging cable and a light-duty tool cable are judged very differently, and a supplier who asks what your cable has to survive is usually thinking along the right lines.
Give the Supplier the Whole Cable Structure
Outer diameter alone is not enough for a serious quotation. Conductor count, strand gauge, jacket thickness and hardness all change how a cable responds to heat and tension. A thin, soft-jacketed cable and a thick, stiff one can both be “about 5 mm” and need completely different settings. Buyers who share the full cable construction at the enquiry stage tend to get more realistic answers, and often catch a mismatch before any money moves.
Batch Variation Is Real, and Honest Suppliers Say So
Insulation compound is not perfectly identical from one batch to the next, and its response to heat shifts a little with it. No winding machine removes that variable completely. What a well-run process gives you is a workable window and a way to adjust inside it. If a supplier claims their machine produces identical results regardless of material batch, treat that as a reason to ask more questions. If they explain how settings are adjusted when the material changes, that usually reflects real production experience.
Where Supplier Background Shows Up
As a Guangdong Xiezhan manufacturer, our winding equipment work grew out of heating element production, where pitch stability and tension control are unforgiving and any drift shows up in the product almost immediately. That habit carries into cable forming: tension and heat are treated as things to measure and verify, not settings to adjust by feel.
As a Guangdong Xiezhan factory, we would rather run your cable through a trial and show you the results than describe the machine in general terms. The XZ-T2301 is the model most conversations start with, though the right configuration depends on your cable and your coil diameter. More on how the team works is set out on the about us page.
Reading a Track Record Properly
When a supplier points to past customers, the useful details are practical ones: what kind of cable, how long the equipment has been in service, and what had to be adjusted along the way. A list of company names says very little on its own. Examples of how equipment has been matched to different production requirements are outlined on the client cooperation page, and that level of detail is what to expect from any supplier you are seriously considering.
A Few Questions Buyers Ask at This Stage
Can one machine handle both PU and PVC cable?
Usually yes within a defined range, but the heat and hold settings differ. Confirm the changeover process and test both materials rather than assuming.
How many stretch cycles should a sample survive?
That depends on the end use. Agree the target with your own customer first, then test to it, instead of relying on a supplier’s general figure.
Should I send my own cable for the trial run?
Yes. Your actual cable structure is the only reliable test, since conductor build and jacket hardness change how it responds to heat and tension.
Does a larger coil diameter make forming harder?
It can. Larger coils are harder to hold in shape during cooling and more sensitive to tension variation, so mention your target diameter range early.
Is a heat-setting stage always required?
For most PU spiral cable, a heated and cooled forming stage is what gives the coil its lasting shape. If a supplier proposes skipping it, ask how the coil will hold its form over time.
If you are weighing a spring cable winding machine against a specific cable, sending the full cable construction and your target coil diameter through contact us will get a far more useful reply than a general enquiry.